Where One Term Ends and the Next Begins, Part 4 of 7: Test Uncertainty Ratio (TUR) - A Screen, Not a Decision Rule
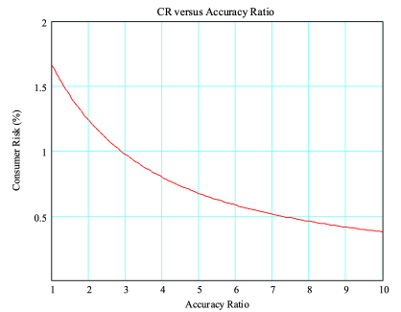
Figure 7. Consumer risk against accuracy ratio. The curve passes through roughly 1 % consumer risk near a 3:1 ratio, the relationship Hayes worked on.
Jerry Hayes of the United States Navy had a problem in the mid-1950s. Measurement decision risk had been worked out on paper by Eagle, Grubbs, and Coon, and almost nobody could use it. There was no computing power to speak of. So, Hayes accepted a consumer's risk of about 1 % and worked out that roughly a 3:1 accuracy ratio would deliver it. Assuming a 95 % confidence level for each, Hayes used specifications for the test ratio: the numerator was the unit under test's specifications, and the denominator the calibration standards' specifications. The intent was to use procedure controls to mitigate other measurement errors during testing. Not fully trusting that all specifications were equal, Hayes and Crandon increased the ratio to 4:1. Three became four. The Navy adopted 4:1, and much of the metrology community followed. The 4:1 rule therefore provides a specific level of risk only under explicit assumptions and conditions.
That rule was always meant as a placeholder until the math got easier. The math got easier decades ago. Yet, the placeholder is still on purchase orders, and some argue to keep the 4:1 TAR rule. TAR, Test Accuracy Ratio, is not a typo for TUR: the original rule compared accuracy specifications, not uncertainties, because specifications were what was simple to use at the time. In some fairness, many manufacturers of metrology equipment lived on reputation in those days, so their specifications were taken at face value.
What TUR Is
The Test Uncertainty Ratio is the tolerance of the item under test divided by the expanded uncertainty of the calibration process. ILAC-G8 writes it as TUR = TL/U. ANSI/NCSL Z540.3 writes the same thing with the span of a symmetric tolerance over twice the expanded uncertainty. JCGM 106 and UKAS LAB 48 call it the measurement capability index, Cm, and LAB 48 defines C95 = (TU − TL)/(2·U95). For a symmetric tolerance, every one of those gives the same number.
The denominator is where labs go wrong. It is not the reference standard's accuracy; that was the old Test Accuracy Ratio, and it ignored everything else. It is the whole calibration process uncertainty: the reference's CMC, the unit under test's resolution and repeatability, the environment, and the other contributors, combined in quadrature, excluding only the unit's own bias. ILAC-P14 asks for the same contents on the certificate. If your TUR denominator is smaller than your certificate uncertainty, you have calculated a TAR and called it a TUR.
What TUR Does
TUR answers one question: is this measurement process capable enough to make the decision at all? It is a screening ratio, and it screens at the population level. Dobbert's managed guardband work, and the Reese and Harben paper that followed it, showed that at a TUR of 4.6:1 or better the worst-case global false accept risk stays below 2 % with no guardband at all. That is useful. It is what UKAS LAB 48 means when it says the role of uncertainty under simple acceptance is to act as a precondition: PASS when the value is within tolerance AND C95 ≥ 5, FAIL otherwise.
What TUR Does Not Do
It does not change the risk of the one decision in front of you. Picture the measurement result as a bell curve centered on the observed value, with its width set by the uncertainty. Move that curve so its center sits exactly on the tolerance limit. Half the area is outside. The specific probability that this item is actually out of tolerance is about 50 %, and it is 50 % at a TUR of 2:1, at 4:1, and at 10:1. A higher TUR narrows the curve, so fewer results land close enough to the limit for this to matter, and the guardband needed to control the risk gets smaller. But at the limit, the coin flip is the coin flip.
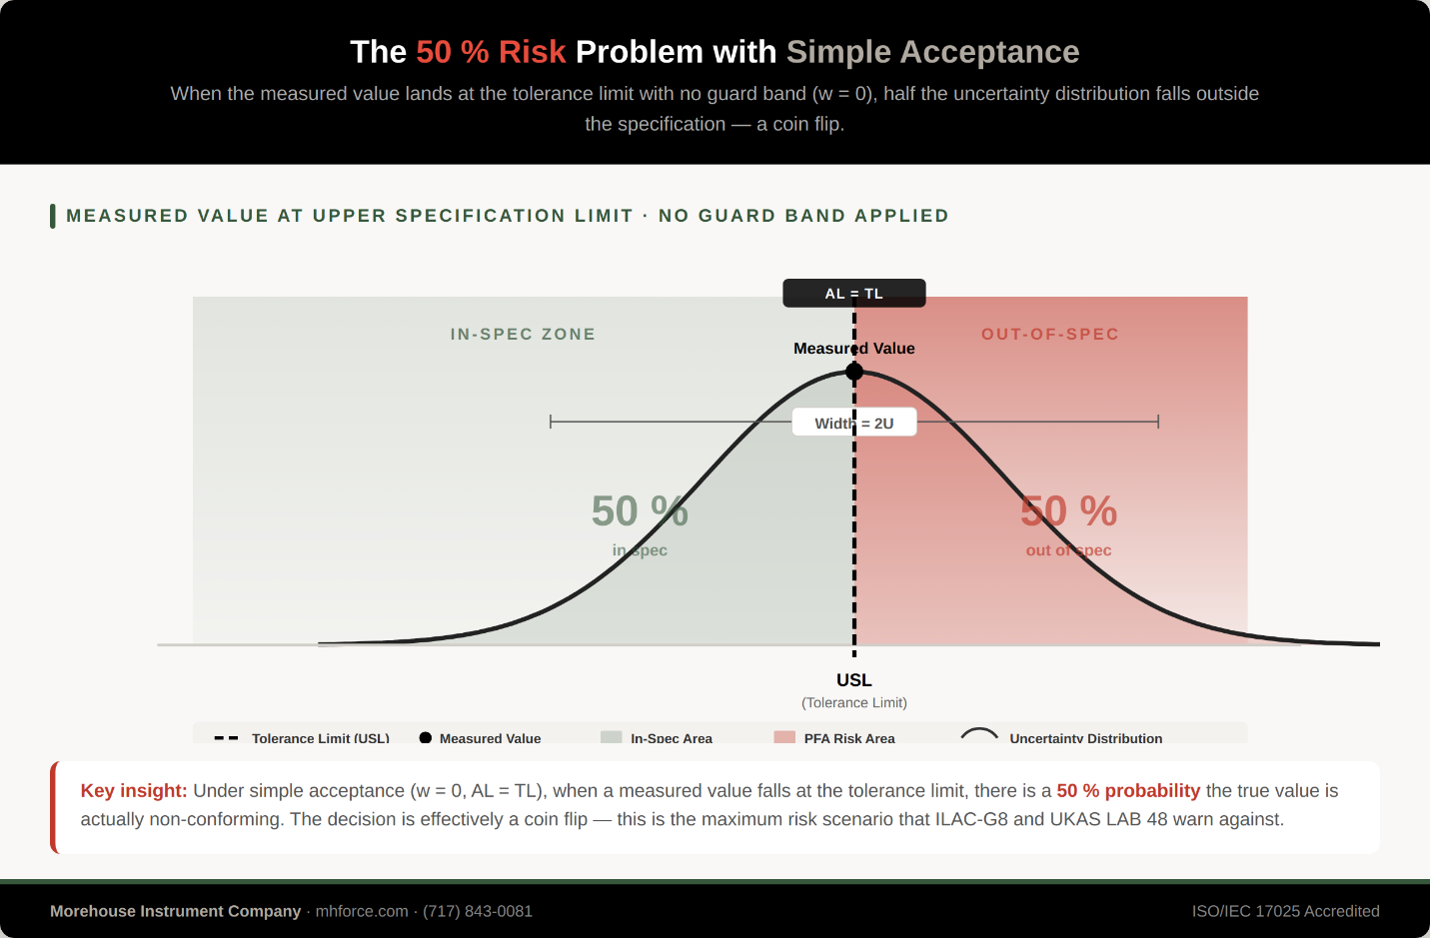
Figure 8. The 50 % problem. Under simple acceptance, a measured value exactly at the tolerance limit has half its distribution outside the specification, whatever the TUR.
That coin flip has a name: simple acceptance, often called shared risk. The measured value is reported, no guardband is applied (w = 0), and anything at or inside the tolerance passes. ISO/IEC 17025 permits it only when the rule is explicitly defined and agreed with the customer, and the customer accepts a probability of false acceptance that can reach 50 % at the tolerance limit. The standard does not prescribe an acceptable risk level; it requires that the risk be understood and documented.
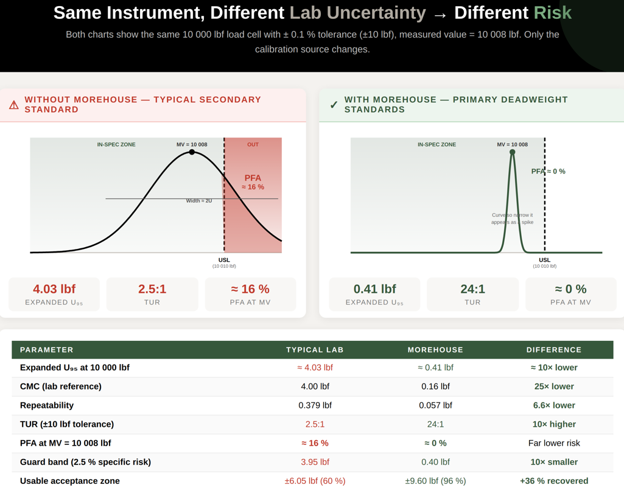
Figure 9. Same instrument, same tolerance, same measured value of 10 008 lbf. Only the calibration source changes, and with it the uncertainty, the TUR, the guardband, and the usable acceptance zone.
Here is the same load cell, the same ±0.1 % tolerance on 10 000 lbf, the same measured value of 10 008 lbf, under two calibration sources. Against a secondary standard, U ≈ 4.03 lbf, k = 2, and the TUR is about 2.5:1. The curve spills past the upper limit, and the specific PFA at 10 008 lbf is about 16 %. To pull that below 2.5 % you need a guardband of about 3.95 lbf, which eats nearly 40 % of the tolerance and leaves an acceptance zone of ±6.05 lbf. Against deadweight primary standards, U ≈ 0.41 lbf, k = 2, the TUR is about 24:1, the guardband shrinks to about 0.40 lbf, and the acceptance zone is ±9.60 lbf, almost the full specification. The TUR did not make the decision. It set how much of the tolerance you get to keep.
TUR Is One of Two Doors, Not the Only One
There is a second route to the same 2 % global target, and it has nothing to do with TUR. NASA HDBK 8739.19-4 Annex 4 and the paper Using Reliability to Meet Z540.3's 2 % Rule show that if the end-of-period reliability for a family of like instruments is 89 % or better, the unconditional false accept risk across that population stays at or below 2 % whatever the measurement uncertainty. Our Start With the End in Mind paper calls these the dual dominance conditions: bench-level dominance at TUR ≥ 4.6:1, global dominance at EOPR ≥ 89 %. Either one alone is sufficient. That is why a lab with a modest TUR and good reliability records can meet a Z540.3 program requirement, and why a lab with a superb TUR and no records still has to compute the guardband. The two doors open onto the same room, and both are population statements. Neither changes the specific risk of the result at 10 008 lbf.
The Boundary
TUR is an input to the decision rule, and sometimes a precondition inside it. It is never the rule. Specifying TUR ≥ 4:1 on a purchase order with no decision rule tells the lab how capable to be and tells it nothing about how to treat a result at 10 008 lbf. The Decision Rule Guidance puts it this way: a stated TUR is a global risk control. Specific risk governs the correctness of an individual pass/fail decision. Both are legitimate. They answer different questions.
TUR ≥ 4:1 by itself is a wish. UKAS LAB 48 writes simple acceptance rules the same way: measurement uncertainty enters as a pre-condition that must be met before the acceptance decision, and its example rule reads PASS when the measured value is within tolerance and the capability constraint is met, FAIL otherwise.
-Henry Zumbrun, Morehouse Instrument Company
References
Sources cited across Parts 1 through 7, listed alphabetically. JCGM documents follow the citation form the BIPM recommends, with the member-organization author line and the JCGM DOI. Clause numbers given in the text refer to these editions.
A2LA. R205 — Specific Requirements: Calibration Laboratory Accreditation Program. American Association for Laboratory Accreditation, Frederick, MD.
ANSI/NCSL Z540.3-2006 (R2013). Requirements for the Calibration of Measuring and Test Equipment. NCSL International, Boulder, CO, 2006.
ASME B89.7.4.1-2005. Measurement Uncertainty Conformance Testing: Risk Analysis. The American Society of Mechanical Engineers, New York, 2005.
ASTM E74-18. Standard Practices for Calibration and Verification for Force-Measuring Instruments. ASTM International, West Conshohocken, PA, 2018. https://doi.org/10.1520/E0074-18
BIPM. The BIPM key comparison database (KCDB). Bureau International des Poids et Mesures, Sèvres. https://www.bipm.org/kcdb/
BIPM, IEC, IFCC, ILAC, ISO, IUPAC, IUPAP and OIML. Evaluation of measurement data — Guide to the expression of uncertainty in measurement. Joint Committee for Guides in Metrology, JCGM 100:2008. https://doi.org/10.59161/JCGM100-2008E
BIPM, IEC, IFCC, ILAC, ISO, IUPAC, IUPAP and OIML. Evaluation of measurement data — The role of measurement uncertainty in conformity assessment. Joint Committee for Guides in Metrology, JCGM 106:2012. https://doi.org/10.59161/JCGM106-2012
BIPM, IEC, IFCC, ILAC, ISO, IUPAC, IUPAP and OIML. International vocabulary of metrology — Basic and general concepts and associated terms (VIM), 3rd edition. Joint Committee for Guides in Metrology, JCGM 200:2012. https://doi.org/10.59161/JCGM200-2012
BIPM, IEC, IFCC, ILAC, ISO, IUPAC, IUPAP and OIML. Guide to the expression of uncertainty in measurement — Part 5: Examples. Joint Committee for Guides in Metrology, JCGM GUM-5:2026. https://doi.org/10.59161/JCGMGUM-5-2026
Carroll, L. Alice's Adventures in Wonderland. Macmillan, London, 1865.
Cenker, G., Zumbrun, H. and Shah, D. Decision Rule Guidance. Morehouse Instrument Company, York, PA. https://mhforce.com/documentation-tools/
Dobbert, M. "A Guard-Band Strategy for Managing False-Accept Risk." Proceedings of the NCSL International Workshop & Symposium, Orlando, FL, 2008.
Eagle, A. R. "A Method for Handling Errors in Testing and Measuring." Industrial Quality Control, Vol. 10, pp. 10–15, March 1954.
Grubbs, F. E. and Coon, H. J. "On Setting Test Limits Relative to Specification Limits." Industrial Quality Control, Vol. 10, pp. 15–20, March 1954.
Harris, G. L. "GMP 13 — Good Measurement Practice for Ensuring Traceability." In: Selected Laboratory and Measurement Practices and Procedures to Support Basic Mass Calibrations, NIST IR 6969, National Institute of Standards and Technology, Gaithersburg, MD, 2019.
Hayes, J. L. Factors Affecting Measuring Reliability. U.S. Naval Ordnance Laboratory, Technical Memorandum No. 63-106, Corona, CA, 1955.
ILAC-G8:09/2019. Guidelines on Decision Rules and Statements of Conformity. International Laboratory Accreditation Cooperation, 2019.
ILAC-P14:09/2020. ILAC Policy for Measurement Uncertainty in Calibration. International Laboratory Accreditation Cooperation, 2020.
ISO/IEC 17025:2017. General requirements for the competence of testing and calibration laboratories. International Organization for Standardization, Geneva, 2017.
ISO/IEC 17043:2023. Conformity assessment — General requirements for the competence of proficiency testing providers. International Organization for Standardization, Geneva, 2023.
Mimbs, S. M. "Using Reliability to Meet Z540.3’s 2 % Rule." NCSL International Workshop & Symposium, National Harbor, MD, 2011. NASA KSC-2011-151.
Morehouse Instrument Company. Decision Rules Interactive Calculator. https://decisionrules.mhforce.com
Morehouse Instrument Company. Guidance on Uncertainty Budgets for Force Measuring Devices. York, PA. https://mhforce.com/documentation-tools/
Morehouse Instrument Company. GUM in Plain English (series). York, PA. https://mhforce.com/documentation-tools/
Morehouse Instrument Company. Morehouse CMC Workbook. York, PA. https://mhforce.com/documentation-tools/
Morehouse Instrument Company. Morehouse True Cost Calculator and The True Cost of Measurement Decisions. York, PA. https://mhforce.com/documentation-tools/
Morehouse Instrument Company. Start With the End in Mind. York, PA, 2026. https://mhforce.com/wp-content/uploads/2026/05/Start_With_The_End_in_Mind.pdf
Morehouse Instrument Company. Probability of False Reject (PFR) (webinar). York, PA.
NASA-HDBK-8739.19-4. Estimation and Evaluation of Measurement Decision Risk. NASA Measurement Quality Assurance Handbook, Annex 4. National Aeronautics and Space Administration, Washington, DC, 2010.
NCSL International. Handbook for the Application of ANSI/NCSL Z540.3-2006 — Requirements for the Calibration of Measuring and Test Equipment. NCSL International, Boulder, CO, 2009.
Peart, N. "Freewill." Performed by Rush on Permanent Waves. Anthem Records, 1980.
Reese, P. and Harben, J. "Risk Mitigation Strategies for Compliance Testing." NCSLI Measure, Vol. 7, No. 1, 2012.
UKAS. LAB 48: Decision Rules and Statements of Conformity, Edition 5. United Kingdom Accreditation Service, Staines-upon-Thames, 2024.
About Morehouse
We believe in changing how people think about Force and Torque calibration in everything we do, including, "Where One Term Ends and the Next Begins, Part 4 of 7: Test Uncertainty Ratio (TUR) - A Screen, Not a Decision Rule"
This includes setting expectations and challenging the "just calibrate it" mentality by educating our customers on what matters and what may cause significant errors.
We focus on reducing these errors and making our products simple and user-friendly.
This means your instruments will pass calibration more often and produce more precise measurements, giving you the confidence to focus on your business.
Companies around the globe rely on Morehouse for accuracy and speed.
Our measurement uncertainties are 10-50 times lower than the competition, providing you with more accuracy and precision in force measurement.
We turn around your equipment in 7-10 business days so you can return to work quickly and save money.
When you choose Morehouse, you're not just paying for a calibration service or a load cell.
You're investing in peace of mind, knowing your equipment is calibrated accurately and on time.
Through Great People, Great Leaders, and Great Equipment, we empower organizations to make Better Measurements that enhance quality, reduce risk, and drive innovation.
With over a century of experience, we're committed to raising industry standards, fostering collaboration, helping with understanding risk, and delivering exceptional calibration solutions that build a safer, more accurate future.
Contact Morehouse at info@mhforce.com to learn more about our calibration services and load cell products.
Email us if you ever want to chat or have questions about a blog.
We love talking about this stuff. We have many more topics other than, "Where One Term Ends and the Next Begins, Part 4 of 7: Test Uncertainty Ratio (TUR) - A Screen, Not a Decision Rule"
Our YouTube channel has videos on various force and torque calibration topics here.